

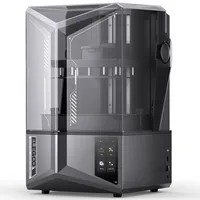
The Elegoo Saturn 4 Ultra is a large-format mono LCD MSLA printer aimed at enthusiasts and semi-professionals who demand 12K resolution, fast cure times and a 219×123×220 mm build platform, without sacrificing detail. Its tilt-release mechanism reduces peel forces for faster, more reliable prints compared to classic FEP designs.
What it is
The Saturn 4 Ultra uses a monochrome LCD panel with 12K resolution and roughly 10-inch diagonal, yielding a pixel pitch of approximately 19 µm. MSLA technology (Masked Stereolithography Apparatus) cures an entire layer at once, so layer time depends only on the UV exposure setting rather than model size. The tilt-release mechanism peels each layer without sharp vertical pulls, which is critical for high-viscosity resins and fragile lattice structures. The printer is aimed at wargaming miniaturists, dental and jewellery professionals, and anyone for whom precision matters more than raw throughput.
Technical specifications
| Technology | Mono LCD / MSLA (UV 405 nm) |
|---|---|
| Build volume | 219 × 123 × 220 mm |
| Screen resolution | 12K (11520 × 6480 px) |
| LCD size | ~10 inches (diagonal) |
| Pixel pitch | ~19 µm (XY) |
| Release mechanism | Tilt-release |
| Class / Price | Hobbyist · ~€430 |
Who it’s for
- Miniatures and figurines (wargaming) (The 12K panel captures muscle striations, rivets and sub-0.1 mm sword edges) ideal for Warhammer, DnD and collector figurines (Hobby and tabletop gaming)
- Dental models and surgical guides: the large platform allows printing a full arch or 8–10 individual models simultaneously at clinically acceptable accuracy (Dental medicine)
- Jewellery masters and wax positives: Castable wax and castable resins produce precise positive patterns for direct burnout and casting in gold, silver and platinum (Jewellery and goldsmithing)
Setup and calibration
- Level the build plate against the FEP: loosen the plate locking screws, lower it to the zero position with a paper sheet or use the printer's guided levelling wizard, then tighten the screws evenly. Uniform pressure across the entire plate area ensures first-layer adhesion and prevents skewed or tilted bases.
- Run an exposure calibration test (Cones of Calibration or RERF): print a standardised test matrix with incrementally increasing UV exposure and select the level at which cones are well-defined and fine lines show no merging. Optimal exposure level for the specific resin and layer thickness, no under-exposure (parts falling off) or over-exposure (loss of precision).
- Inspect the FEP / nFEP film: hold it up to light, hazy, matte patches or cracks indicate a worn film. Replace when accumulated print time exceeds ~15 hours or upon visible damage. A clear, transparent film transmits UV uniformly, directly affecting layer detail and ensuring layers cure onto the resin rather than sticking to the FEP.
- Monitor resin level and temperature: fill the vat to the marked MAX line, and before printing confirm the resin is at least 20–25 °C (optimally 25–30 °C), use a heater mat or warm water bath if needed. Cold or insufficient resin causes uneven curing, FEP sticking and adhesion failure, particularly on cupped geometries with large cross-sections.
Common defects and fixes
Resin exposure helper
Pick a resin type for starting exposure values (typical for mono-LCD machines). These are STARTING points: always run an exposure test, because the exact seconds depend on your screen power and the specific resin:
Conclusion
The Saturn 4 Ultra is a serious tool for anyone who needs both a large platform and micron-level precision. Its 12K panel and tilt-release mechanism make it competitive in the €400 segment, while broad resin compatibility opens it to dental, jewellery and miniature applications. Proper platform levelling and exposure calibration account for 90% of success: invest that time once and you will be collecting perfect prints consistently.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert