

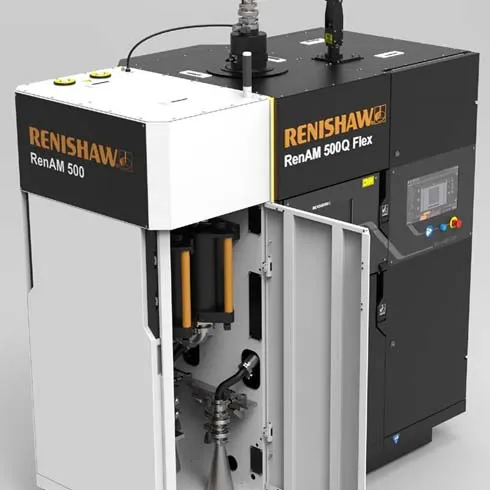
The Renishaw RenAM 500 is an industrial metal LPBF (Laser Powder Bed Fusion) printer designed for the production of high-quality metal components with exceptional repeatability. With a 250×250×350 mm build volume, up to four 500 W fibre lasers, and the integrated InfiniAM solution for real-time process monitoring, the RenAM 500 is the preferred choice for aerospace manufacturing, medical implants, and precision tooling.
What it is
The RenAM 500 is a series of LPBF machines from Renishaw: a company with over 50 years of experience in metrology and precision engineering. The series includes the Q model (four lasers for maximum throughput), the S model (single laser for research and small batches), and the Flex (easy powder changeover for multi-material work). Renishaw's key advantage is its closed powder system: powders are loaded, recycled and discharged without manual contact, ensuring safe operation and high inter-build powder consistency. The integrated InfiniAM monitoring detects melt-pool anomalies in real time, enabling in-process validation of every built part. The RenAM 500 series machines are qualified for use in regulated industries, including AS9100 (aerospace) and ISO 13485 (medical devices).
Technical specifications
| Technology | LPBF: Laser Powder Bed Fusion (SLM/DMLS) |
|---|---|
| Build volume | 250 × 250 × 350 mm |
| Laser system | 1–4 × 500 W Yb fibre laser (model dependent) |
| Process monitoring | InfiniAM Spectral + InfiniAM Central (real-time melt-pool) |
| Powder system | Closed-loop, with automated sieving and recycling |
| Inert atmosphere | Argon or nitrogen; O₂ < 0.1% |
| Class / Price | Industrial · ~€750,000 |
Applications and industries
- Medical implants and dental prosthetics: production of patient-specific orthopaedic implants (hip, spinal, cranial) and dental crowns/bridges from Ti6Al4V and CoCr with biocompatible surfaces and complex trabecular porous structures for osseointegration (Medical and dental)
- Aerospace structural components: building lightweight topology-optimised structural parts from Inconel 718/625 and Ti6Al4V: brackets, fuel nozzles, heat exchangers with internal channels, under AS9100 quality control and InfiniAM traceability (Aerospace and defence)
- Precision tooling with conformal cooling: manufacturing of injection moulds and tool inserts from maraging steel and tool steel with conformal cooling channels that follow the mould profile exactly, reducing injection-moulding cycle time by 20–40% (Mould-making and plastics processing)
Production workflow
- Preparation: load certified powder into the closed system, confirm O₂ ≤ 0.1%, and set build parameters (layer thickness, laser power, scan speed) in QuantAM. Safe, inert atmosphere with correct parameters, minimal risk of oxidation or porosity.
- LPBF build with InfiniAM monitoring: the machine builds the part layer by layer; InfiniAM Spectral records melt-pool intensity and flags anomalies (pores, cracks) in real time. Full traceability of every layer; anomalies are detected during the process, not after it.
- Heat treatment and part removal: remove the build platform, stress-relieve in a furnace, then cut parts from the platform by EDM or bandsaw. Reduced residual stresses; parts are ready for subsequent machining.
- Finishing and inspection: CNC or EDM finishing of functional surfaces, HIP (Hot Isostatic Pressing) for critical parts, CMM/CT verification with Renishaw metrology. Parts ready for use, with documented mechanical properties and full traceability back to the powder certificate.
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The RenAM 500 represents Renishaw in metal: a company whose DNA is precision and traceability. The closed powder system, InfiniAM real-time monitoring, and AS9100/ISO 13485 compliance make this machine the preferred choice for organisations where every component must be demonstrably good: not just visually good. For aerospace, medical, and precision tooling applications, the RenAM 500 sets the standard for process control in metal LPBF.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert