

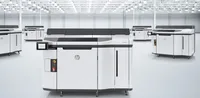
The HP Jet Fusion 5200 is an industrial MJF system built for serial production of polymer parts – high throughput, isotropic mechanical properties and automated powder management. With a 380×284×380 mm build volume and voxel-level precision, it is the choice of manufacturers seeking consistent, end-use nylon components at industrial scale.
What it is
Multi Jet Fusion (MJF) is a technology developed by HP in which two types of agent – a Fusing Agent and a Detailing Agent – are precisely jetted onto a bed of polymer powder. Infrared lamps then pass over the layer and heat only the Fusing Agent zones to sintering temperature, while the Detailing Agent cools the boundaries to produce sharp, accurate edges. The process is exceptionally fast and uniform: the entire powder layer is processed simultaneously, with no moving laser beam. The result is parts with isotropic properties – strength is virtually equal across all axes – a clear differentiator from FDM or SLA parts. The HP Jet Fusion 5200 adds an automated powder management system (loading, recycling, sieving) and integration with a Processing Station, making it suitable for continuous production with no manual intervention between cycles.
Technical specifications
| Technology | MJF – agent jetting + IR sintering of polymer powder |
|---|---|
| Build volume | 380 × 284 × 380 mm |
| Voxel resolution | 1200 dpi (voxel printing) |
| Powder management | automated – loading, recycling, sieving (Processing Station) |
| Mechanical properties | isotropic – equal across all axes |
| Class / Price | Industrial · ~€350 000 |
Applications and industries
- Serial production of end-use parts – Manufacturing hundreds to thousands of identical nylon components with repeatability and isotropic mechanical properties, without the need for tooling or molds (Industrial manufacturing and consumer goods)
- Complex lattices and lightweight structures – Printing topology-optimized and lattice geometries impossible with traditional methods, reducing weight while maintaining strength (Aerospace and medical devices)
- Automotive and consumer components – Production of functional housings, brackets, ducts and custom parts with high strength and good chemical resistance directly from digital file (Automotive and mass consumer market)
Production workflow
- Preparation and nesting: load polymer powder (fresh + recycled, refresh rate ~20–30%), arrange parts in the Build Unit at maximum density using nesting software (HP SmartStream or 3rd-party) to minimize powder cost and cycle time. Optimized powder bed with uniform density and minimal material waste relative to refresh ratio.
- MJF printing: the Build Unit enters the printer and an automated cycle starts – Fusing Agent and Detailing Agent are jetted layer by layer, IR lamps sinter each layer; no manual intervention is required during printing. Fully sintered parts embedded in a powder cake with uniform density and no inter-layer deformation.
- Powder cake cooling: after printing ends, the Build Unit is transferred to the Processing Station for controlled cooling – do not open before reaching safe temperature (typically 3–12 hours depending on fill density). Gradual cooling prevents thermal stress and warping of thin-walled or asymmetric parts.
- Unpacking, bead blasting and post-processing: excavate parts from the powder cake, recycle unsintered powder, bead-blast surfaces to remove residue; optionally – vibratory tumbling, dyeing or impregnation for improved surface finish and color. Clean, ready-to-use parts with uniform surface; dyeing (standard black or grey) masks the typical grey color of PA12.
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The HP Jet Fusion 5200 is a machine for production environments where repeatability, speed and isotropic part properties are non-negotiable. MJF erases the boundary between prototyping and serial manufacturing – the same parameters deliver one or a thousand identical parts. Long cooling times and powder management requirements make the investment meaningful at sufficient volume, but for the right application the Jet Fusion 5200 does not compete with traditional methods – it replaces them.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert