

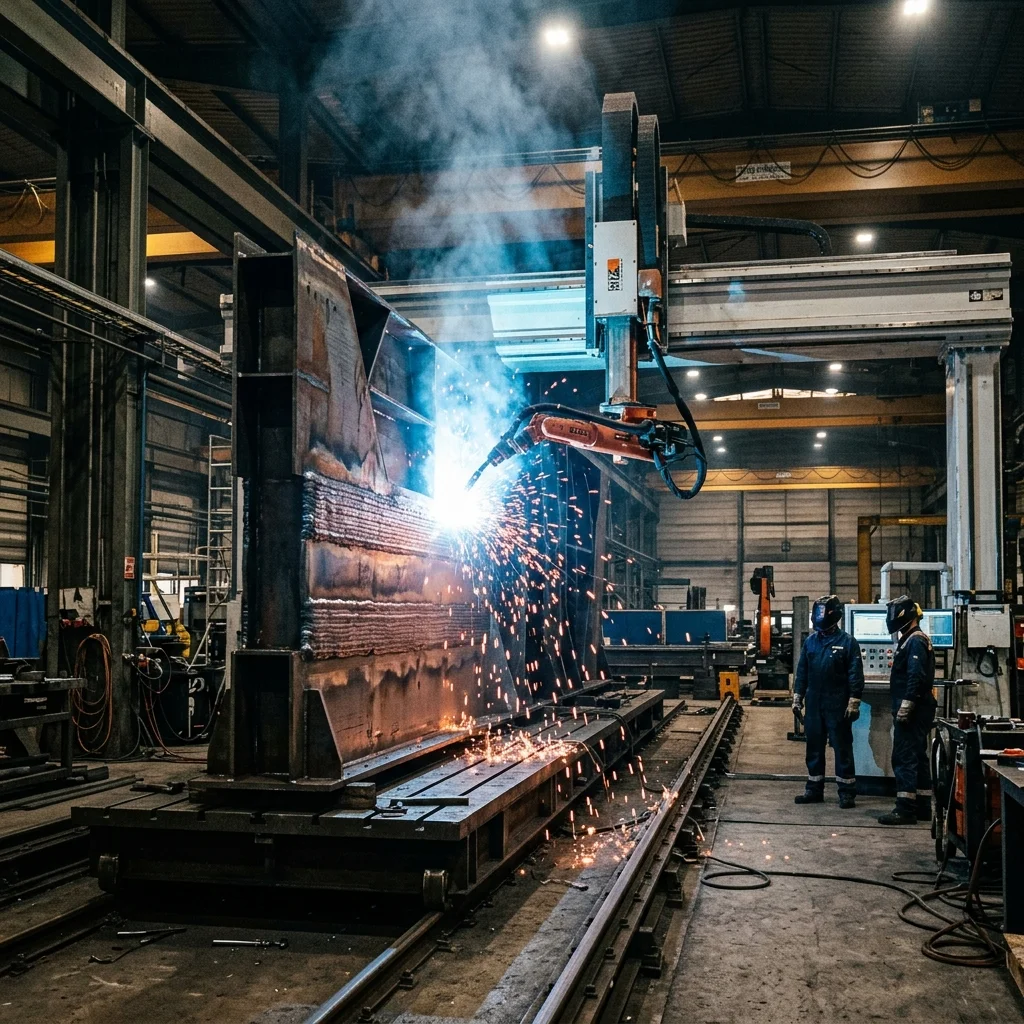
In 2025–2026, Wire Arc Additive Manufacturing (WAAM) has emerged as the dominant technology for producing large-scale metal components. While powder-bed fusion (PBF) excels at fine-featured parts, WAAM uses electric arc welding and metal wire feedstock to deposit steel, titanium, and aluminum at rates of 1–5 kg/hr, producing parts measured in meters, not millimeters.
Operating Principle: MIG/MAG Welding + CNC Positioning
WAAM is a Directed Energy Deposition (DED) process combining standard welding equipment with robotic or CNC positioning:
System Components
- Welding Source: MIG/MAG (GMAW), TIG (GTAW), or CMT (Cold Metal Transfer). Fronius CMT is preferred for WAAM due to its low heat input.
- Metal Wire (Feedstock): Standard welding wire, ER70S-6 (mild steel), ER308L (stainless steel), ER4043 (aluminum), ERTi-2 (titanium).
- Shielding Gas: Argon, CO₂, or Ar/CO₂ mixtures (for steel). Protects the melt pool from oxidation.
- Robot or CNC Gantry: 6-axis industrial robot (e.g., KUKA, ABB, Fanuc) or large CNC gantry for weld head positioning.
Process
- The robot deposits molten metal along pre-programmed paths, with each layer 1–3 mm tall and 3–8 mm wide.
- Deposition rate is 1–5 kg/hr (for steel), significantly faster than PBF (0.1–0.5 kg/hr).
- Parts up to 2 × 2 × 2 meters (and larger with gantry systems) can be produced.
Interactive Filament Selector
Answer 3 quick questions and find the optimal material for your project.
1. What are the mechanical requirements for the part?
2. What temperature will the part operate at?
3. Are there any specific environmental requirements?
Our recommendation:
PLA filament
Ideal for easy printing, model visualization and decorative parts.
Mechanical Properties of WAAM Steel (ER70S-6)
| Property | WAAM ER70S-6 | Rolled Steel S355 | Cast Iron |
|---|---|---|---|
| Ultimate Tensile Strength | 500 – 550 MPa | 470 – 630 MPa | 340 MPa |
| Yield Strength | 380 – 420 MPa | 355 MPa | 210 MPa |
| Elongation at Break | 22% – 28% | 20% – 22% | 12% |
| Impact Toughness (Charpy V) | 60 – 120 J | 27 J (min.) | 10 J |
| Density | 7.85 g/cm³ | 7.85 g/cm³ | 7.2 g/cm³ |
Key Insight: WAAM steel exhibits isotropic mechanical properties (unlike FDM polymers) because full wire melting ensures metallurgical bonding between layers. After normalizing heat treatment (900°C), properties are comparable to or exceed conventional rolled steel.
Challenges and Solutions
1. Residual Stress and Distortion
- Problem: Repeated heating and cooling of each layer generates cumulative thermal stresses that distort the part.
- Solution: Symmetric deposition strategies, inter-layer cooling, and post-build stress relief annealing (580–650°C for steel).
2. Surface Roughness
- Problem: WAAM parts have roughness Ra = 0.5 – 2.0 mm (yes, millimeters, not microns!).
- Solution: CNC machining of functional surfaces. WAAM creates a near-net-shape (NNS) form that is finish-machined.
3. Porosity
- Problem: Hydrogen from moisture, oil, or contaminated wire creates gas pores.
- Solution: Wire drying, high-purity shielding gas (99.99% Ar), optimized parameters.
Pros and Cons
Pros:
- Scale: Multi-meter parts impossible for PBF.
- High Deposition Rate: 1–5 kg/hr (steel), 10× faster than PBF.
- Low Feedstock Cost: Standard welding wire (€5–15/kg) vs. metal powder (€50–200/kg).
- Accessible Equipment: Standard welding robot (~€50,000–150,000) vs. PBF machine (~€500,000–2,000,000).
Cons:
- Low Resolution: Minimum wall width ~3 mm, minimum feature ~5 mm.
- Mandatory Post-Machining: CNC machining required for all functional surfaces.
- Residual Stress: Requires careful thermal cycle management.
- Limited Geometric Complexity: Cannot produce fine lattice structures or internal channels.
Frequently Asked Questions (FAQ)
Waam: Wire Arc Additive Manufacturing For Large Steel Structures Calculator
Interactive optimization calculator.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert