

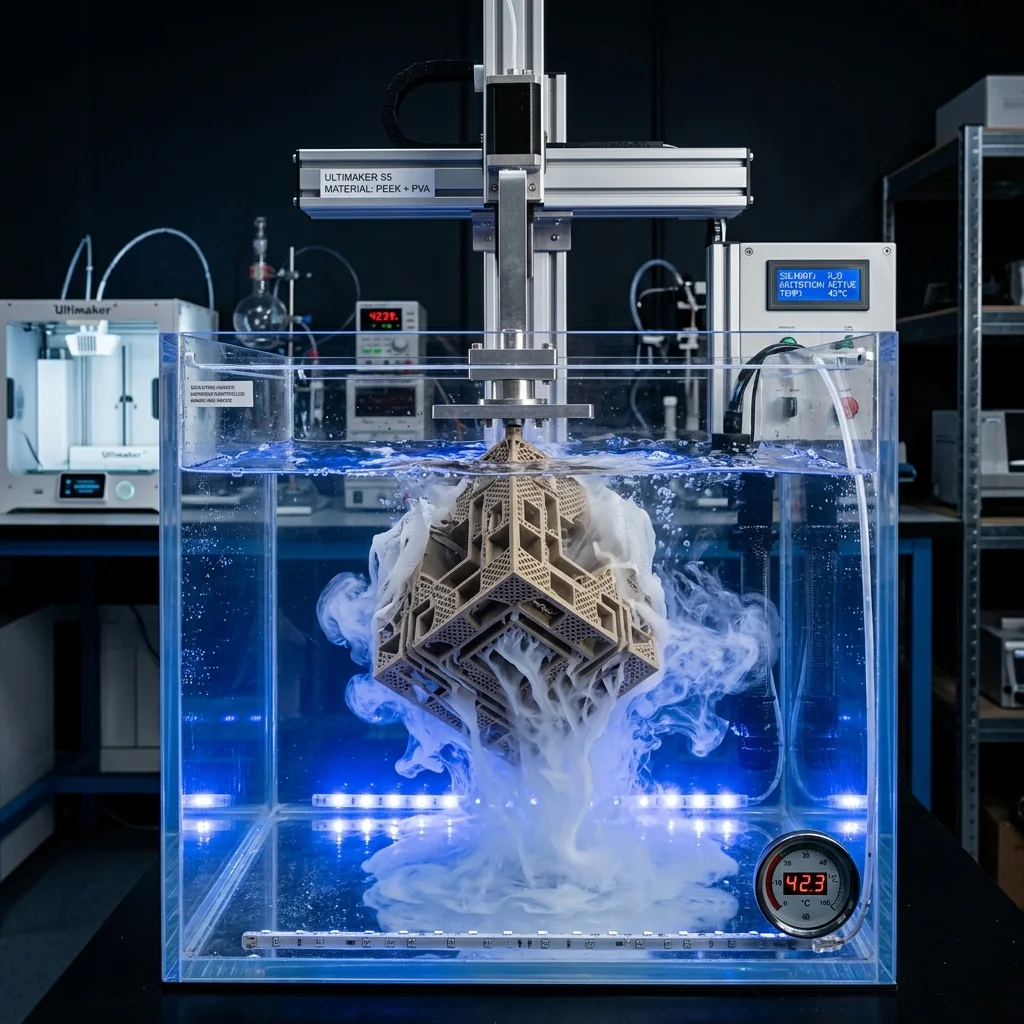
In 2025–2026, high-performance polymers like PEEK and PEI (Ultem) have become standard for structural industrial components. However, printing complex geometries with internal cavities or overhanging features requires support structures.
Traditional water-soluble support materials like PVA and BVOH degrade thermally long before they reach the extrusion temperatures of superpolymers, demanding specialized high-temperature water-soluble support materials.
The Thermodynamic Challenge
Printing PEEK requires extrusion temperatures of 380°C to 400°C and an active heated chamber temperature exceeding 150°C to control the crystallization kinetics of the semi-crystalline matrix.
- Thermal Destruction of PVA/BVOH: Standard Polyvinyl Alcohol (PVA) degrades at temperatures above 200°C. In a nozzle heated to 380°C, PVA immediately carbonizes, causing severe, irreversible hot-end clogs.
- Chamber Collapse: Even if they survive extrusion, standard support materials will soften and sag under their own weight in a 150°C chamber due to their low glass transition temperatures ($T_g < 60^circ ext{C}$).
High-Temperature Soluble Supports (HT Soluble Supports)
Modern HT soluble supports (such as AquaTek X1 or modified sulfonated co-polyesters) are engineered to withstand extreme thermal conditions:
- Thermal Stability: These materials feature heat deflection temperatures (HDT) exceeding 150°C–180°C and can withstand extrusion temperatures up to 340°C–360°C without chemical degradation.
- Dissolution Chemistry: They dissolve in warm water or mild alkaline solutions. Water molecules hydrate the polar groups along the polymer chain, breaking intermolecular attractions and converting the solid polymer into a soluble colloid.
- Advantage Over Breakaway Supports: Mechanically breaking away supports from narrow internal channels or complex medical implants is impossible and leaves surface scars. HT soluble supports dissolve completely, ensuring clean internal structures and dimensional accuracy.
Material Comparison: Soluble Supports for High-Temperature Polymers
| Property | HT Soluble Support (AquaTek X1) | BVOH | Breakaway Support (HT) |
|---|---|---|---|
| Max Extrusion Temperature | 350°C – 360°C | 210°C – 230°C | 380°C – 400°C |
| HDT (Deflection Temp) | >= 150°C | ~55°C | > 180°C |
| Removal Method | Dissolution (Warm water/alkaline) | Dissolution (Water) | Mechanical breakaway |
| Hygroscopicity | Extremely High | High | Low |
| PEEK/PEI Adhesion | Very Good | Zero adhesion | Very Good |
| Surface Finish | Smooth (No scars) | N/A | Rough scars remaining |
Interactive Filament Selector
Answer 3 quick questions and find the optimal material for your project.
1. What are the mechanical requirements for the part?
2. What temperature will the part operate at?
3. Are there any specific environmental requirements?
Our recommendation:
PLA filament
Ideal for easy printing, model visualization and decorative parts.
Pros and Cons of HT Soluble Supports
Pros:
- Design Freedom: Enables printing of complex fluid manifolds, hollow turbine blades, and patient-specific medical implants.
- Clean Surface Finish: The interfaces where PEEK rests on the support remain smooth and dimensionally accurate.
- Automated Clean-Up: Supports dissolve autonomously in a heated bath with circulating water.
Cons:
- Extreme Hygroscopicity: Absorbs ambient moisture rapidly. Filament must be dried at 80°C for 6–8 hours and fed from a drybox during printing to prevent steam void defects.
- High Cost: HT soluble polymers are highly specialized and carry a high price premium.
- Dual Extrusion Requirement: Requires industrial dual-extrusion printers capable of running independent hot-end profiles (e.g., 400°C for PEEK and 350°C for the support).
Frequently Asked Questions (FAQ)
Interactive Analyzer for Water-Soluble Support Materials For Peek And Pei
Select a profile to view detailed analysis.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert