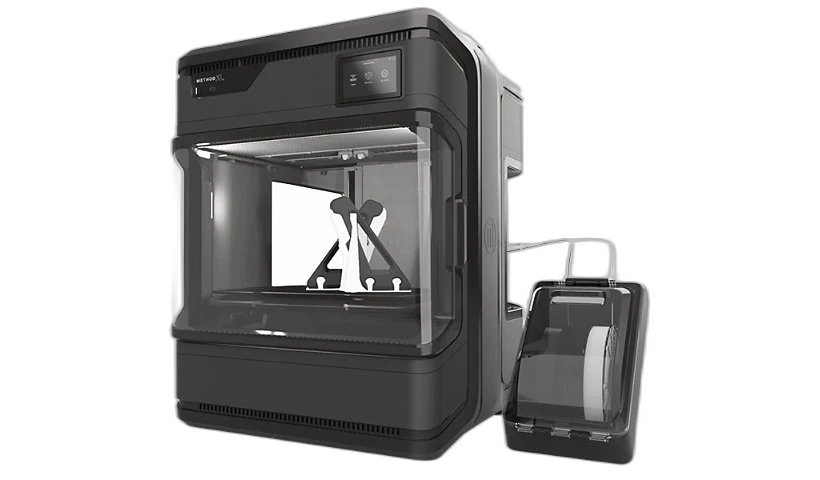
The UltiMaker Method XL is a professional FDM printer with an actively heated chamber up to 100°C and a 305×305×320 mm build volume, engineered for materials that demand a controlled thermal environment. Dual extrusion with soluble supports (RapidRinse/SR-30) and production-grade repeatability make it the go-to tool in industry, aerospace and automotive applications.
What it is
The Method XL is the successor to the MakerBot Method platform, carried over under the UltiMaker brand after the two companies merged. Its defining feature is an actively heated enclosed chamber: unlike the passively warmed chambers found on most desktop printers, here the chamber is held at a constant temperature of up to 100°C throughout the entire print. This eliminates the thermal gradient that causes warping in ABS and Nylon and delivers isotropic mechanical properties approaching those of injection moulding. The machine targets production engineers, R&D departments and manufacturing facilities where part repeatability and quality take priority over speed.
Technical specifications
| Technology | FDM (Fused Deposition Modeling) |
|---|---|
| Build volume | 305 × 305 × 320 mm |
| Chamber | ACTIVELY HEATED: up to 100°C |
| Extrusion | Dual (model + soluble supports) |
| Support materials | RapidRinse and SR-30 (soluble) |
| Class / Price | Industrial · ~€7,500 |
Applications and industries
- Engineering functional parts without warping: printing ABS, Nylon and PC components in a heated chamber up to 100°C that eliminates thermal-gradient warping and delivers repeatable quality (Automotive and aerospace)
- Tooling and production jigs: rapid production of fixtures, templates and clamping jigs from Nylon-CF and ABS, replacing traditionally machined metal parts for short runs (Manufacturing and industrial engineering)
- Low-volume end-use parts: producing end-use parts directly from CAD with soluble supports for complex geometry and no manual support removal after printing (Medical devices and consumer electronics)
Production workflow
- Clean the build plate with isopropyl alcohol (IPA) and verify even application of the adhesive layer. A degreased surface guarantees maximum first-layer adhesion for engineering materials.
- Activate chamber pre-heating and wait for the set temperature (up to 100°C) to be reached before starting the print. A stabilised chamber eliminates warping and delivers isotropic mechanical properties throughout the entire volume.
- Run automatic bed levelling and fine-tune the Z-offset. A correctly positioned first layer with no elephant's foot or corner detachment.
- Run a Flow Tower test for the model and soluble support extruders separately. Precise extrusion from both heads: no wall gaps and no excess at support interfaces.
- Submerge the finished print in the solvent (water for RapidRinse, or d-limonene for SR-30) and verify complete support dissolution. Clean final-part geometry with no support remnants, ready for direct use.
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The UltiMaker Method XL is the right choice when repeatability, dimensional accuracy and the mechanical properties of engineering polymers are non-negotiable. The actively heated chamber up to 100°C makes warping in ABS and Nylon practically impossible, and dual extrusion with soluble supports unlocks complex geometry without manual post-processing. The price is high, but with the right business case the machine pays for itself through saved machining and manual labour.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert
Updated on 11 September 2026
This article was written with AI assistance; the facts were checked against the sources on 11 September 2026.