

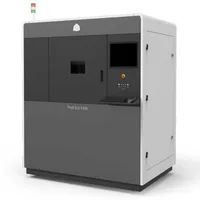
The 3D Systems ProX SLS 6100 is an industrial SLS machine for serial production of polymer parts without support structures. With a 381×330×460 mm build volume, automated powder handling and a heated build chamber, the ProX SLS 6100 turns laser sintering of nylon into a managed production process.
What it is
The ProX SLS 6100 operates on the principle of selective laser sintering (SLS): a CO₂ laser scans cross-sections over a powder layer, fusing particles together, then the platform drops by one layer thickness and the process repeats. Without support structures, the powder bed itself retains the geometry. The machine is designed for a production environment: the closed system for recycling and blending powder (virgin + refresh) reduces material waste, while automated loading and unloading minimize manual labor between cycles. The result: functional end-use parts with isotropic mechanical properties and complex internal geometries impossible with traditional methods.
Technical specifications
| Technology | SLS (Selective Laser Sintering): CO₂ laser |
|---|---|
| Build volume | 381 × 330 × 460 mm |
| Laser | CO₂, 100 W |
| Layer thickness | 0.08 – 0.15 mm |
| Powder handling | automated: loading, blending and recycling of powder |
| Heated chamber | yes: controlled temperature for uniform sintering |
| Class / Price | Industrial · ~€300 000 |
Applications and industries
- Functional end-use parts (serial production of strong nylon components with complex geometry, directly from machine to assembly) no tooling required (Industrial manufacturing and consumer goods)
- Aerospace and automotive components: lightweight brackets, ducts and chassis parts with topology optimization, meeting stringent mechanical and thermal requirements (Aerospace and automotive)
- Durable series batches (producing hundreds of identical parts in one cycle with repeatable mechanical properties) suitable for medical devices, sporting goods and industrial automation (Medical devices and sporting goods)
Production workflow
- Preparation: load and condition the powder. Powder (virgin + recycled at the correct ratio) is homogeneous and at operating temperature, guaranteed density and sintering repeatability.
- SLS sintering: the laser scans layer by layer inside the heated chamber. Controlled chamber temperature minimizes thermal gradients, parts free of distortion and with isotropic properties.
- Cooldown: wait for the controlled cool-down of the powder cake. Slow, uniform cooling prevents residual stress and warping, parts retain their dimensional accuracy.
- Depowdering and finishing: extract parts and remove powder with bead blasting or vibratory systems. Clean surface ready for direct use or post-processing (dyeing, impregnation, metallization).
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The ProX SLS 6100 is the choice for manufacturers who need repeatable, automated production of strong polymer parts with complex geometry, without compromising between the throughput of serial production and the precision of the detail. Automated powder handling reduces operating costs, the heated chamber ensures isotropic properties, and the broad materials portfolio covers needs from aerospace to medical.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert