

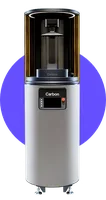
The Carbon M2 is an industrial DLP printer operating on Carbon's patented CLIP (Continuous Liquid Interface Production) technology, also known as DLS (Digital Light Synthesis). Unlike layer-by-layer resin printers, CLIP uses a continuous light process with an oxygen-based "dead zone" beneath the growing part, delivering substantially faster throughput and fully isotropic mechanical properties.
What it is
The M2 is Carbon's production flagship: a machine designed not for prototyping but for real series production of end-use parts. Carbon's two-component thermoset resins (A-component + B-component catalyst) are mixed immediately before filling the resin tray, and after printing the parts must go through a thermal post-cure (bake) in an oven to complete polymerization and reach the designed mechanical properties. The result is parts with isotropic strength, without the weak horizontal layer boundaries typical of conventional SLA/DLP machines. The M2 operates exclusively within Carbon's Software-as-a-Service subscription ecosystem.
Technical specifications
| Technology | DLP / CLIP-DLS (continuous liquid interface production) |
|---|---|
| Build volume | 189 × 118 × 326 mm |
| Material system | two-component thermoset Carbon resins (A+B component) |
| Post-processing | mandatory thermal post-cure (bake) in SpeedCell oven |
| Mechanical properties | isotropic: no Z-axis weakness |
| Business model | SaaS subscription: hardware + cloud + materials + support |
| Class / Price | Industrial · ~€50,000 |
Applications and industries
- High-volume end-use production (series production of functional polymer components with repeatability unattainable for conventional SLA) automotive brackets, housings, fasteners (Automotive and industrial mechanics)
- Athletic midsoles and custom insoles (custom lattice midsoles for footwear and insoles with controlled cushioning using Carbon EPU and FPU resins) proven production use with Adidas (Sports industry and medical)
- Dental and medical devices (dental splints, prosthetic components and surgical guides from Carbon DPR (Dental Resin)) biocompatible with sub-100 μm accuracy (Dental medicine and surgery)
Production workflow
- Mix and load the two-component resin (A+B component) into the cartridge immediately before starting. Properly mixed resin at the correct ratio ensures complete polymerization and designed mechanical properties.
- CLIP printing: the platform continuously rises upward while the DLP light engine cures the resin from below, and the oxygen dead zone prevents adhesion to the window. The continuous process eliminates layer boundaries and reduces print time by up to 10× compared to conventional SLA.
- Wash the printed parts with isopropyl alcohol (IPA) in the SpeedCell wash unit to remove uncured resin. Clean surfaces free of residual uncured resin, ready for thermal post-cure.
- Thermal post-cure (bake) in the SpeedCell oven at material-specific temperature and time (e.g. 120–180°C for 10–30 min). Completed polymerization of the two-component resins: parts reach final strength, thermal resistance and isotropic properties.
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The Carbon M2 is a production platform rather than a printer in the traditional sense: CLIP/DLS technology, isotropic parts and the integrated SaaS ecosystem position it for companies seeking direct digital manufacturing of end-use parts. Two-component resins and mandatory thermal post-cure demand a disciplined production workflow, but deliver mechanical properties unreachable by standard photopolymer printers.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert