

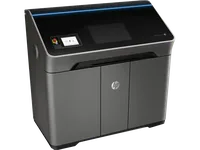
The HP Jet Fusion 580 Color is an industrial MJF machine that does what no other powder-bed technology can: it prints fully functional nylon parts with full-color voxel textures in a single production cycle. Color and mechanical strength at the same time, with no post-print dyeing.
What it is
The Jet Fusion 580 Color runs HP Multi Jet Fusion technology with a color layer added: infrared energy sinters the powder bed layer by layer while the Fusing Agent and Detailing Agent control melting, and dedicated color agents deposit CMYK texture directly at the voxel level. The result is a PA12 (Nylon 12) part with predictable mechanical properties and a full-color surface: achievable only with systems in the HP 580 Color class. The machine targets design studios, medical devices, consumer products and any industry where visual identity matters as much as function. Important: the HP Jet Fusion 580 (without Color) does not carry the color agents, the distinction is fundamental, not merely commercial.
Technical specifications
| Technology | MJF: Multi Jet Fusion with full-color voxel printing |
|---|---|
| Build volume | 332 × 190 × 248 mm |
| Color printing | CMYK voxel texture embedded directly in the part |
| Primary material | PA12 (Nylon 12): color-primed |
| Resolution | 600 dpi (XY), layer 0.08 mm |
| Powder refresh rate | ~70 % new powder (higher than 5200 series) |
| Class / Price | Industrial · ~€55 000 |
Applications and industries
- Full-color functional prototypes (verifying form, color and ergonomics in a single printed part) without manual painting or post-print texture application (Industrial design and consumer goods)
- Anatomical and medical models with color coding (surgical models with color-coded tissues, vessels and organs) functional PA12 material resistant to steam sterilization (Medical devices and education)
- Consumer products with embedded color and branding: housings, handles, orthotic aids and personalized accessories with full-color branded graphics, durable for everyday use (Consumer goods and personalization)
Production workflow
- Nest parts in the build unit with at least 5 mm clearance and plan orientation for even color texture coverage. Maximum build density and prevention of color cross-contamination between adjacent parts.
- Verify the color profile (ICC / HP SmartStream) and review the color texture simulation in SmartStream 3D Build Manager before launch. Confirmed color reproduction accuracy and early detection of clipped or distorted textures.
- Launch the MJF color print cycle: the machine deposits Fusing Agent, Detailing Agent and CMYK color agents layer by layer under IR heating. Sintered PA12 parts with embedded full-color voxel texture and uniform mechanical properties throughout.
- Allow the full Build Unit cooling cycle to complete (minimum 2–3 hours, recommended with the Fast Cooling Unit). Warping and residual thermal stress distortion prevented by premature extraction.
- Depowder, clean with air blast or bead blasting, then apply HP Color Sealing Agent for long-term color retention. Vibrant, stable colors resistant to UV and daily use; powder is recycled back into the system.
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The HP Jet Fusion 580 Color occupies a unique niche in industrial 3D printing: the only MJF platform that delivers full-color voxel texture on mechanically sound PA12 parts in a single cycle. Unlike the HP Jet Fusion 580 (without Color), the 580 Color is the right choice when color is a functional requirement: not decoration. The trade-offs are a higher powder refresh rate and mandatory sealing for lasting color, but for design-driven industries and medical visualization this machine has no direct competitor in its class.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert