

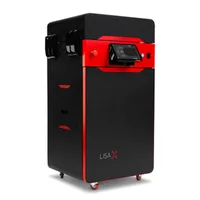
The Sinterit Lisa X is a benchtop SLS machine built for production-grade small series and functional polymer parts. With an IR laser, a larger build chamber (130×180×330 mm) and nitrogen atmosphere support, the Lisa X bridges the gap between lab prototyping and real production flexibility, at under €20,000.
What it is
The Lisa X is the successor to the Lisa Pro in Sinterit's lineup: faster, with a larger chamber and an infrared laser replacing the CO₂ technology of older models. SLS (Selective Laser Sintering) requires no support structures: the powder surrounding the part acts as self-support, enabling complex geometries and nested packing of multiple parts in a single run. The Lisa X is an open system: it works with Sinterit's own materials but also accepts certified third-party powders. Nitrogen atmosphere reduces oxidation during sintering and improves the mechanical properties of finished parts. Compared to the Lisa Pro, the Lisa X offers 43% more build volume, higher scan speed and more efficient thermal control: placing it firmly in the production-grade benchtop SLS class.
Technical specifications
| Technology | SLS: Selective Laser Sintering |
|---|---|
| Build volume | 130 × 180 × 330 mm |
| Laser | IR laser (infrared) |
| Atmosphere | nitrogen (N₂): reduced oxidation |
| Material system | open: Sinterit + certified third-party powders |
| Class / Price | Production benchtop · ~€18,000 |
Applications and industries
- Functional small-series production (producing 1–200 end-use parts per run through nested packing) no supports, no tooling, no minimum order quantity (Medical devices and consumer goods)
- Flexible and elastomeric components: TPU powder enables printing of soft gaskets, orthopaedic insoles and shock-absorbing geometries directly from CAD (Healthcare and sports equipment)
- Durable engineering prototypes: PA12 and PA11 deliver final-material parts: not visual mock-ups, for form, fit and load testing under real conditions (Automotive and aerospace)
Production workflow
- Prepare and weigh the powder: blend fresh and recovered powder at the recommended Refresh Rate ratio. Homogeneous bulk density and correct thermal behaviour, the foundation for even sintering.
- Load powder into the chamber and close the system; when using nitrogen, activate the N₂ purge. An inert atmosphere prevents yellowing and polymer degradation during sintering.
- Wait for the chamber thermal equilibration: the machine heats the powder bed to the set temperature just below the melting point (around 168–172°C for PA12). Stable temperature prevents distortion, warping and uneven porosity in the parts.
- Start the print: the IR laser scans each layer, followed by the roller depositing a fresh powder layer. Parts form layer by layer inside the powder cake, with no support structures needed.
- Cool slowly: let the powder cake cool in a controlled manner (typically 1–2 h for a full chamber) before opening. Rapid cooling causes distortion and internal stresses. Slow cooling preserves geometric accuracy.
- Unpack and clean the parts: remove unsintered powder with a brush or bead-blaster and recover it for the next cycle. Recovered powder is blended with fresh powder per the Refresh Rate formula, near-zero production waste.
Key considerations
Materials and applications
Pick a material/alloy this machine processes to see its properties and typical applications:
Conclusion
The Sinterit Lisa X is the right choice when you need production-grade SLS on a benchtop: a larger chamber, faster IR laser and nitrogen support make it significantly more capable than the Lisa Pro without exceeding a €20,000 budget. No support structures, an open material system and near-zero powder waste make it economically compelling for runs of 1–200 parts in PA12, PA11, TPU or PP.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert