

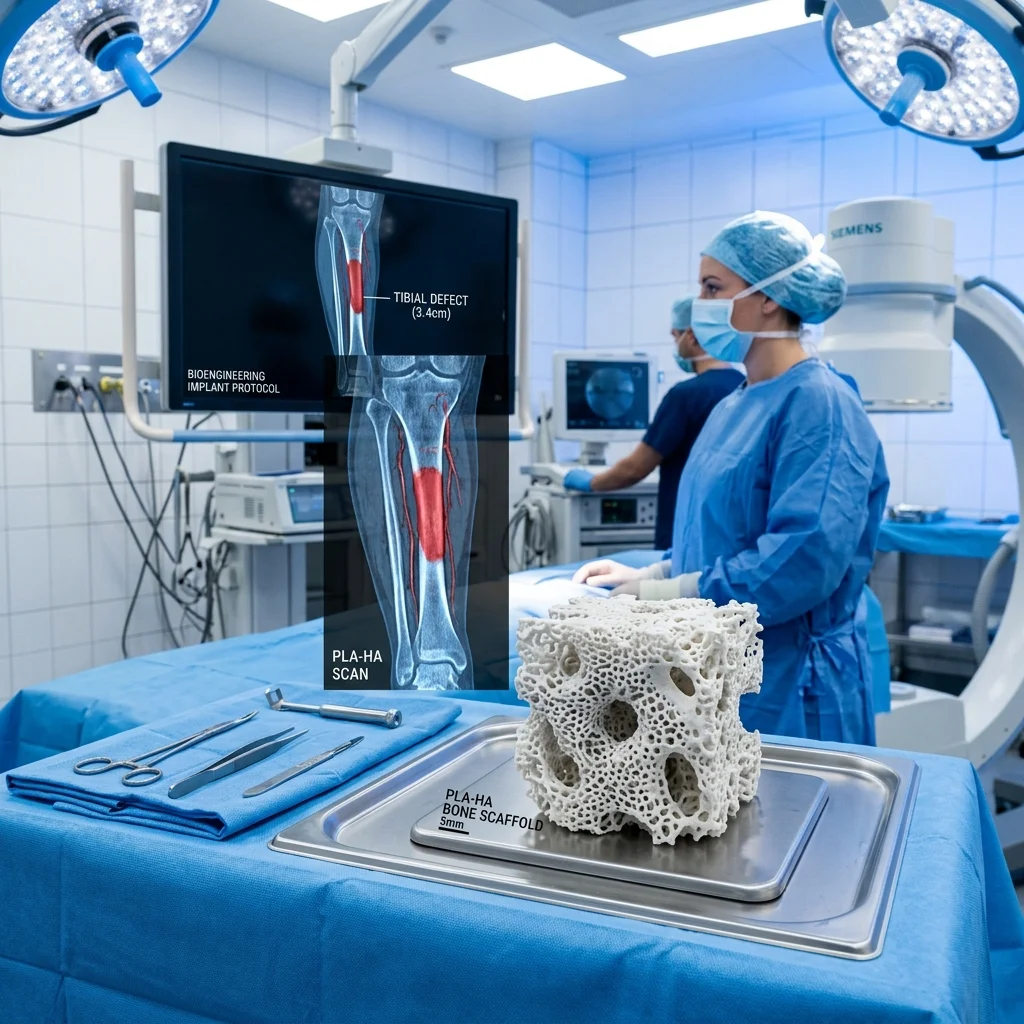
In 2025–2026, the intersection of additive manufacturing and regenerative medicine has produced a new class of bioactive composites. PLA-Hydroxyapatite (PLA-HA) composites combine a biodegradable polylactide matrix with the primary mineral component of human bone (hydroxyapatite ($Ca_{10}(PO_4)_6(OH)_2$)) to create scaffolds that are gradually replaced by living bone tissue.
This article examines the biochemistry of osteoconduction, optimal print parameters, and the regulatory landscape for medical-grade 3D-printed implants.
Biochemistry: Why Hydroxyapatite Stimulates Bone Growth
Hydroxyapatite (HA) constitutes approximately 65–70% of the mass of natural bone. When HA nanoparticles are embedded in a polymer matrix, they interact with the biological environment through three mechanisms:
1. Osteoconduction
HA surfaces serve as a “bridge” for osteoblast migration (bone-forming cells). The porous scaffold architecture provides a 3D template along which bone cells migrate and deposit new mineralized tissue.
2. Bioactivity
Upon contact with body fluids (Simulated Body Fluid: SBF), the HA surface forms a carbonate apatite layer chemically identical to biological bone mineral. This layer creates a direct chemical bond between the implant and living bone (osseointegration).
3. Controlled Biodegradation
The PLA matrix undergoes hydrolysis in the body over 6–24 months (depending on molecular weight and crystallinity). Degradation products (lactic acid) are metabolized naturally. As PLA degrades, the growing bone tissue progressively replaces the scaffold: the ideal scenario for regenerative medicine.
Interactive Filament Selector
Answer 3 quick questions and find the optimal material for your project.
1. What are the mechanical requirements for the part?
2. What temperature will the part operate at?
3. Are there any specific environmental requirements?
Our recommendation:
PLA filament
Ideal for easy printing, model visualization and decorative parts.
Optimal HA Nanoparticle Content
| HA Content (wt%) | Mechanical Effect | Biological Effect |
|---|---|---|
| 5% – 10% | Minimal elastic modulus increase | Moderate improvement in cell adhesion |
| 10% – 20% | Optimal balance: increased stiffness without ductility loss | Strong osteoconduction, rapid cell proliferation |
| 20% – 30% | Significant stiffness increase, reduced elongation | Maximum bioactivity, but increased brittleness |
| > 30% | Drastically reduced tensile strength, filament embrittlement | Particle agglomeration, difficult extrusion |
Optimal Concentration: 10–20 wt% HA nanoparticles. Above 30%, the filament becomes too brittle for FDM and nozzle clogging from agglomerates becomes frequent.
Print Parameters and Safety Protocols
| Print Parameter | Value | Rationale |
|---|---|---|
| Nozzle Temperature | 200°C – 220°C | Higher than standard PLA due to increased melt viscosity from HA particles. |
| Bed Temperature | 50°C – 60°C | Standard adhesion. |
| Extruder Type | Direct Drive | Mandatory, Bowden tubes generate excessive friction with abrasive HA filament. |
| Nozzle | Hardened Steel ≥ 0.4 mm | Abrasive HA nanoparticles will rapidly erode brass nozzles. |
| Print Speed | 15 – 30 mm/s | Slow extrusion ensures uniform HA particle distribution. |
| Sterility | ISO Class 7 Cleanroom | Required for medical applications to prevent contamination. |
Post-Processing for Biomedical Application
- Sterilization: Gamma irradiation (25–40 kGy) or ethylene oxide (EtO). Autoclaving (121°C) is NOT suitable: it exceeds PLA’s $T_g$ and deforms the scaffold.
- Surface Treatment: Plasma treatment or NaOH etching to increase hydrophilicity and improve cell adhesion.
Standards and Regulations
| Standard | Scope |
|---|---|
| ISO 10993 | Biocompatibility, toxicology, sensitization, and implantation tests. |
| ISO 13485 | Quality management system for medical devices. |
| ASTM F2792 | Standard terminology for additive manufacturing. |
| FDA 510(k) | Premarket notification for medical devices in the US. |
Pros and Cons
Pros:
- Bioactivity: HA actively stimulates bone tissue growth.
- Personalization: Scaffolds designed from patient-specific CT/MRI data.
- Controlled Porosity: 3D printing enables precise control over pore size (300–500 μm optimal for bone invasion).
- Biodegradability: PLA matrix is absorbed by the body, no second surgery for implant removal.
Cons:
- Low Mechanical Strength: PLA-HA cannot replace load-bearing bones (femur, tibia). Suitable for cranial, facial, and cancellous defects.
- Abrasiveness: HA particles require expensive hardened steel nozzles.
- Regulatory Barriers: Long and costly FDA/EMA approval process.
- Sterility: Requires specialized manufacturing equipment (cleanroom, sterilization).
Frequently Asked Questions (FAQ)
Eco-Footprint of Pla-Hydroxyapatite (Pla-Ha) For Bioactive Bone Grafts
Calculate saved CO2 emissions.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert