

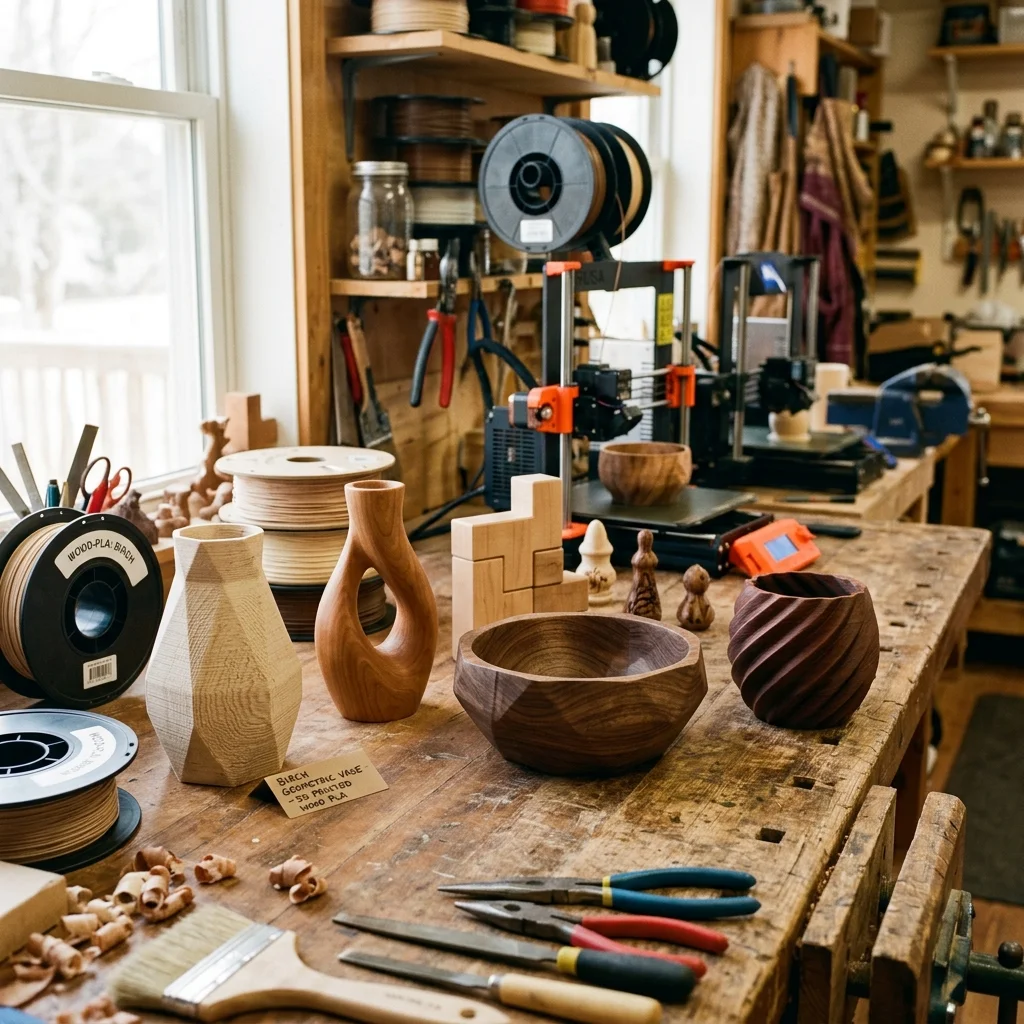
In 2025–2026, aesthetic engineering has advanced with the development of highly realistic organic composites. Wood-Filled Filaments offer a unique capability: simulating real wood grain and ring textures by dynamically altering the extrusion temperature during the printing process.
By understanding the thermal behavior of lignin and cellulose, engineers can generate organic-looking wood components using standard desktop hardware.
The Physics of Color Transition: Lignin Caramelization
Wood-filled filaments typically consist of a PLA base (60% to 80%) blended with fine organic wood fibers or sawdust (20% to 40%) sourced from pine, birch, bamboo, or coconut shell.
The ability to control the color of the printed part relies on the thermal degradation properties of the organic components:
- Lignin & Cellulose: These organic molecules contain complex sugars and carbon ring structures that pyrolyze and char (caramelize) when heated.
- Temperature-Induced Shading: Modifying the hotend temperature alters the degree of carbonization, yielding different shades:
- 180°C – 190°C: Yields a light, blonde wood shade (birch or pine look).
- 210°C – 220°C: Yields a medium brown shade (oak or cherry look).
- 230°C – 240°C: Causes heavy carbonization, resulting in a dark brown tone (walnut or mahogany look).
By running a script that fluctuates the print temperature by $pm5^circ ext{C}$ every few layers, the part emerges with alternating dark and light bands that replicate natural wood grain.
Interactive defect troubleshooting guide
Pick a print defect symptom to see the causes and how to fix it.
Stringing
Possible cause: Damp filament, too high a temperature or too little retraction.
Quick fix:
- Dry the filament for 4-6 hours at 50°C.
- Lower the nozzle temperature by 5-10°C.
- Increase the retraction length by 0.5 to 1.0 mm.
Clogging Risks & Extrusion Physics
Because wood fibers do not melt, they flow as suspended solid particulates inside the liquid polymer stream. This introduces significant rheological challenges:
- Nozzle Diameter: Standard 0.4 mm nozzles are highly susceptible to particulate aggregation (clogging). A 0.5 mm or 0.6 mm nozzle is required to allow the organic fibers to pass freely.
- Retraction Control: Pulling molten plastic back into the cold zone can freeze the fibers and jam the extruder. Retraction distances should be minimized (e.g., < 1.0 mm for Direct Drive systems).
- Temperature Limits: Avoid heating the nozzle above 245°C. At extreme temperatures, the wood fibers will char inside the melt zone, forming hard carbon deposits that require physical clearing.
Post-Processing and Surface Treatment
Since the printed surfaces contain exposed organic cellulose fibers, they interact with post-processing treatments similarly to natural wood:
- Sanding: Easily sanded using standard sandpaper. The layer lines disappear much faster than on pure PLA.
- Staining: The organic fibers absorb wood stains. Applying a dark stain highlights the temperature-induced rings, creating a realistic wood finish.
- Varnishing: Standard wood sealants and oils (like linseed or tung oil) can be applied to protect the part from humidity and enhance color depth.
Pros and Cons of Wood-Filled Composites
Pros:
- Organic Aesthetic: Genuine wood appearance, texture, and organic scent during processing.
- Grain Simulation: Thermal control allows layer-by-layer shading.
- Post-Processability: Can be sanded, stained, and painted like real wood.
- Layer Hiding: The matte, textured surface hides layer lines.
Cons:
- High Clog Risk: Demands larger nozzle diameters and strict retraction management.
- Low Mechanical Strength: Particulate fillers disrupt polymer matrix cohesion, reducing tensile strength. Not suitable for structural, load-bearing parts.
- Brittle Feedstock: The filament is brittle on the spool and can snap easily if fed at sharp angles.
Frequently Asked Questions (FAQ)
M104 S{190 + (layer_num % 12) * 4}. This shifts the temperature between 190°C and 238°C over 12-layer intervals.Wood-Filled Composites: Simulating Real Wood With Variable Temperatures Calculator
Interactive optimization calculator.
The full picture
This article is one page from The Big Book of 3D Printing: 704 illustrated pages covering every technology, material and fix in one reference.
Read it on Kindle →Engineer, author of The Big Book of 3D Printing and additive manufacturing expert