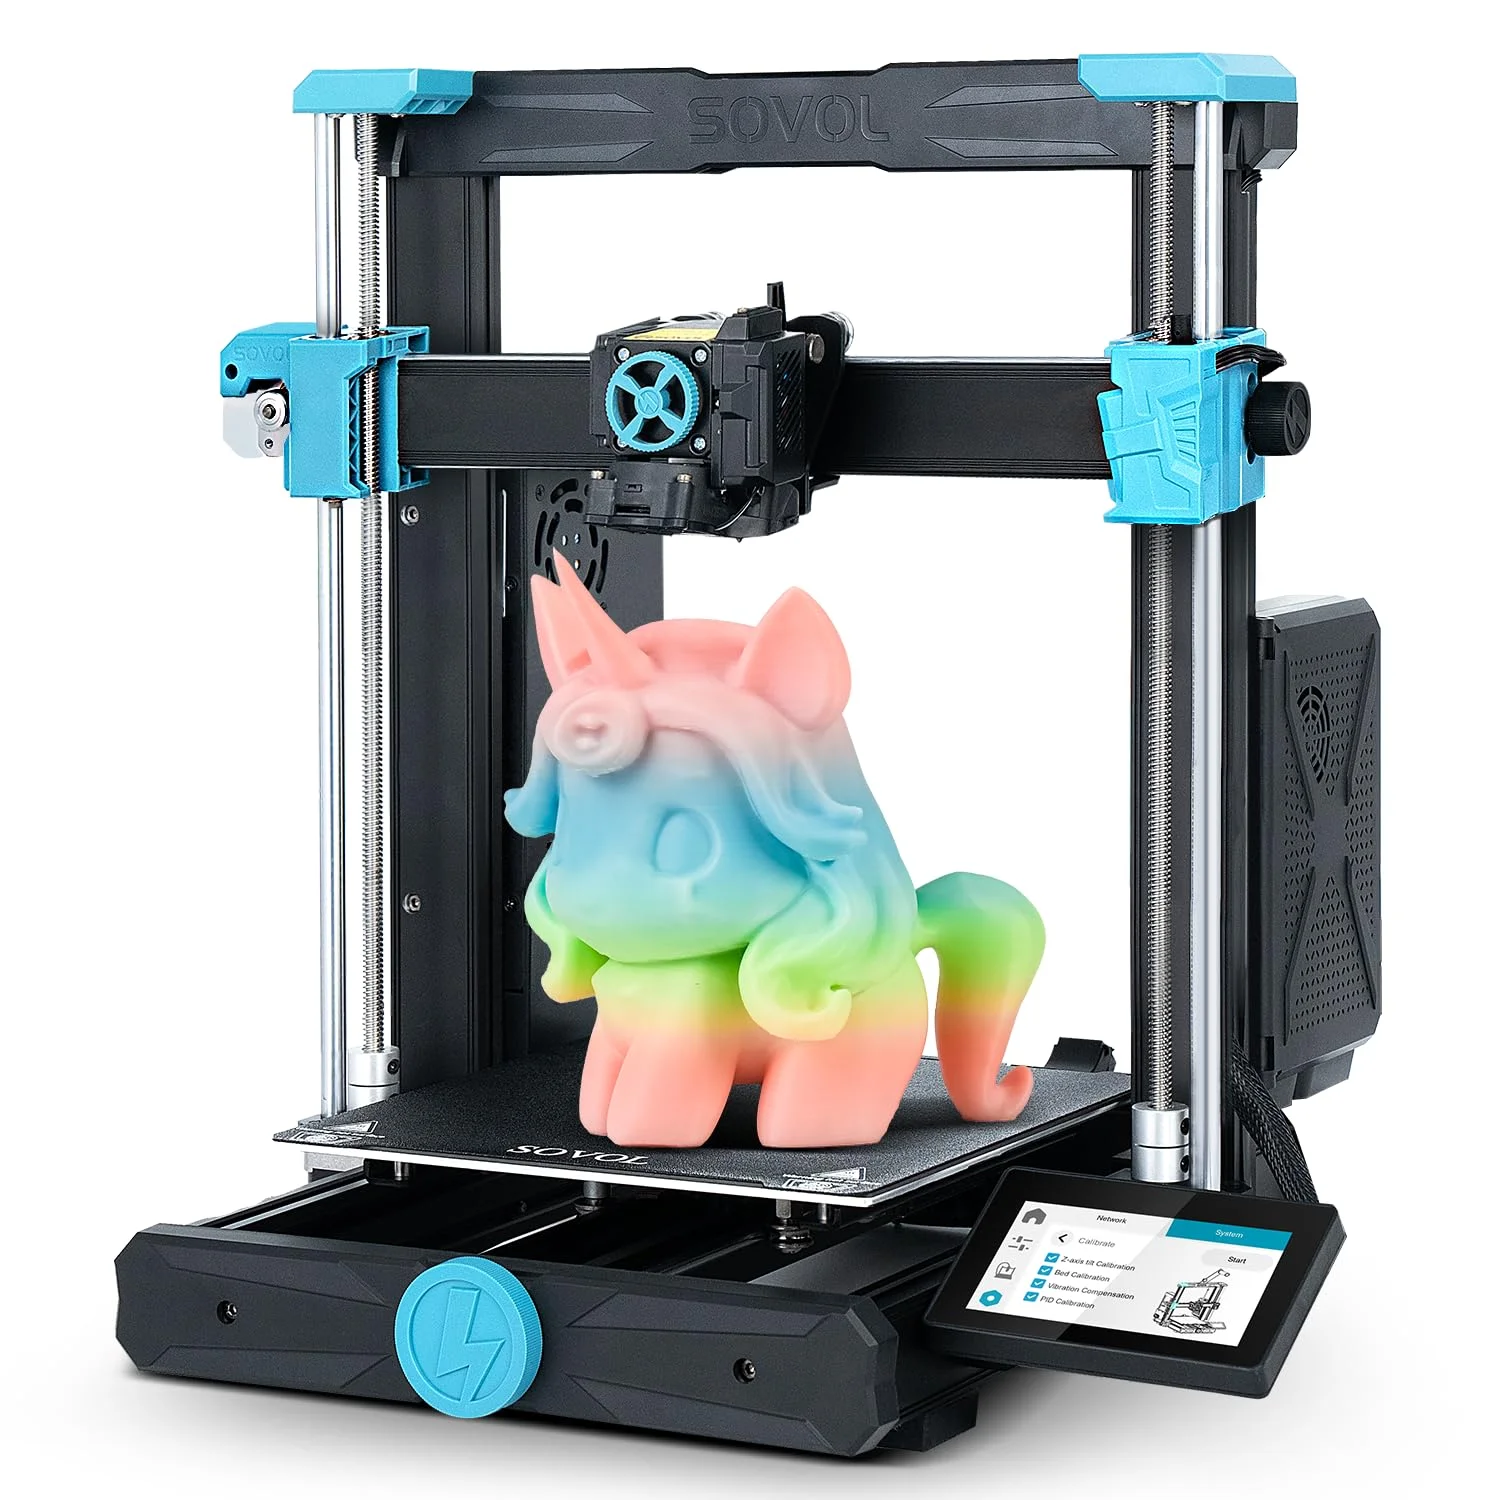
Спецификации
- Производител: Sovol-SV06
- Технология: FDM
- Клас: experimenter
Чести проблеми и решения
Stringing
Appearance of thin plastic threads between distinct parts of the model, caused by hygroscopy (wet filament) or incorrect retraction settings. Решение: Dry the filament (e.g., 4-6 hours at 50°C for PLA). Increase the retraction distance by 1-2 mm, reduce the nozzle temperature by 5°C, and raise the travel speed to 200 mm/s.
Warping
Detachment and upward curling of the model’s corners or edges from the build plate due to uneven thermal contraction. Решение: Clean the bed with IPA, increase its temperature by 5°C, use a Brim (5-10 mm), and reduce the part cooling fan to 30% for the first 5 layers.
Under-extrusion
Formation of thin, brittle walls with gaps due to insufficient material feed, nozzle clogging, or an improperly calibrated extruder. Решение: Perform a Cold pull procedure to clean the nozzle, check the extruder gear tension, and software-calibrate the E-steps (via the M92 command).
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии
Обновено на 21 септември 2026
Този текст е написан с помощта на AI; фактите са сверени с източниците на 21 септември 2026.