
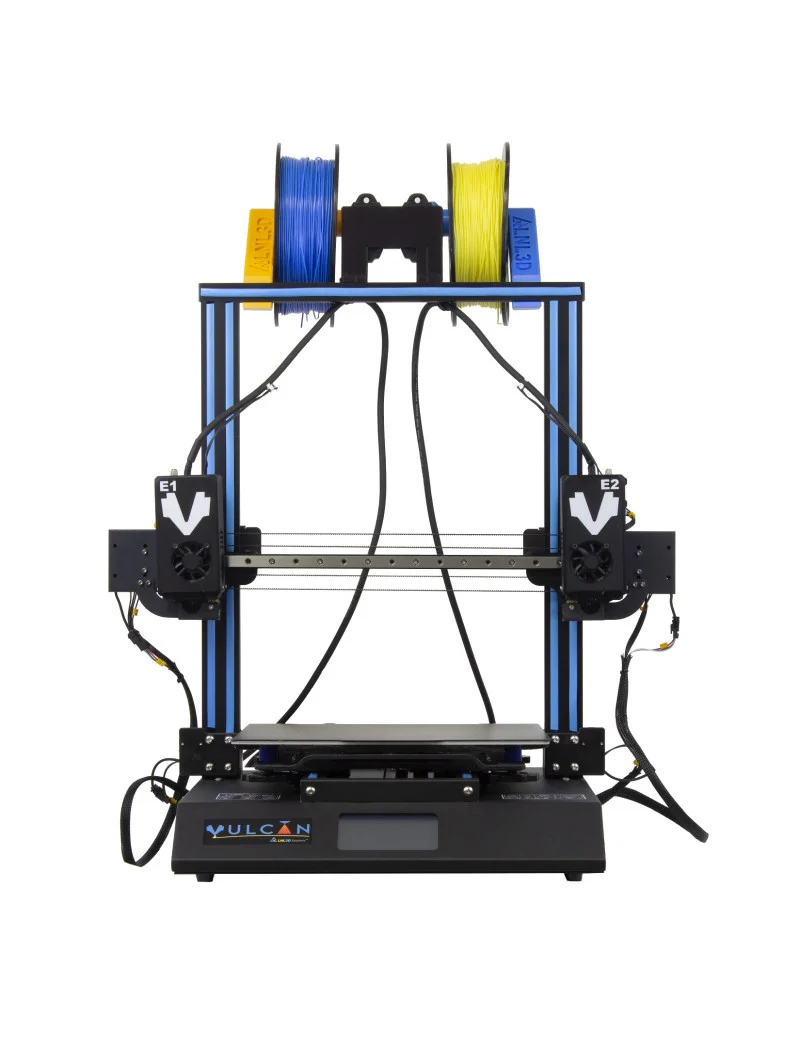
Спецификации
- Производител: LNL3D
- Технология: FDM
- Клас: experimenter
Чести проблеми и решения
Stringing
- Description: Thin plastic threads resembling spiderwebs between printed parts, mostly caused by moisture absorption in the filament. Решение: Dry the filament for 4-6 hours at 50-70°C, increase retraction distance by 1-2 mm, and reduce nozzle temperature by 5°C.
Warping
- Description: Corners or edges of the print detach from the build plate and curl upwards due to uneven cooling and thermal shrinkage. Решение: Increase bed temperature by 5°C, use a Brim or bed adhesive, reduce part cooling fan speed for initial layers, and utilize an enclosure.
Elephant’s Foot
- Description: The bottom layer of the print expands outward beyond the specified CAD dimensions due to excessive squishing against the heated bed. Решение: Raise the Z-offset by 0.05 mm, lower the bed temperature by 5°C for the first layer, and apply a software compensation of 0.1-0.2 mm in the slicer.
Подходящи приложения
- Jigs & Fixtures Manufacturing: Low-volume production of strong, functional manufacturing tools, templates, and fixtures using engineering-grade materials like CF-Nylon.
- Rapid Prototyping: Creating physical models for form, fit, and ergonomic testing within hours to accelerate the product development lifecycle.
- High-Performance Components: Manufacturing critical end-use parts that require exceptional tensile strength and extreme temperature resistance using advanced polymers like PEI (ULTEM).
Интерактивен Анализатор за Lnl3d d3 – спецификации и настройки
Избери профил за да видиш детайлен анализ.
Здравина / Устойчивост
83%
Скорост на принтиране
78%
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии
Обновено на 21 септември 2026
Този текст е написан с помощта на AI; фактите са сверени с източниците на 21 септември 2026.