
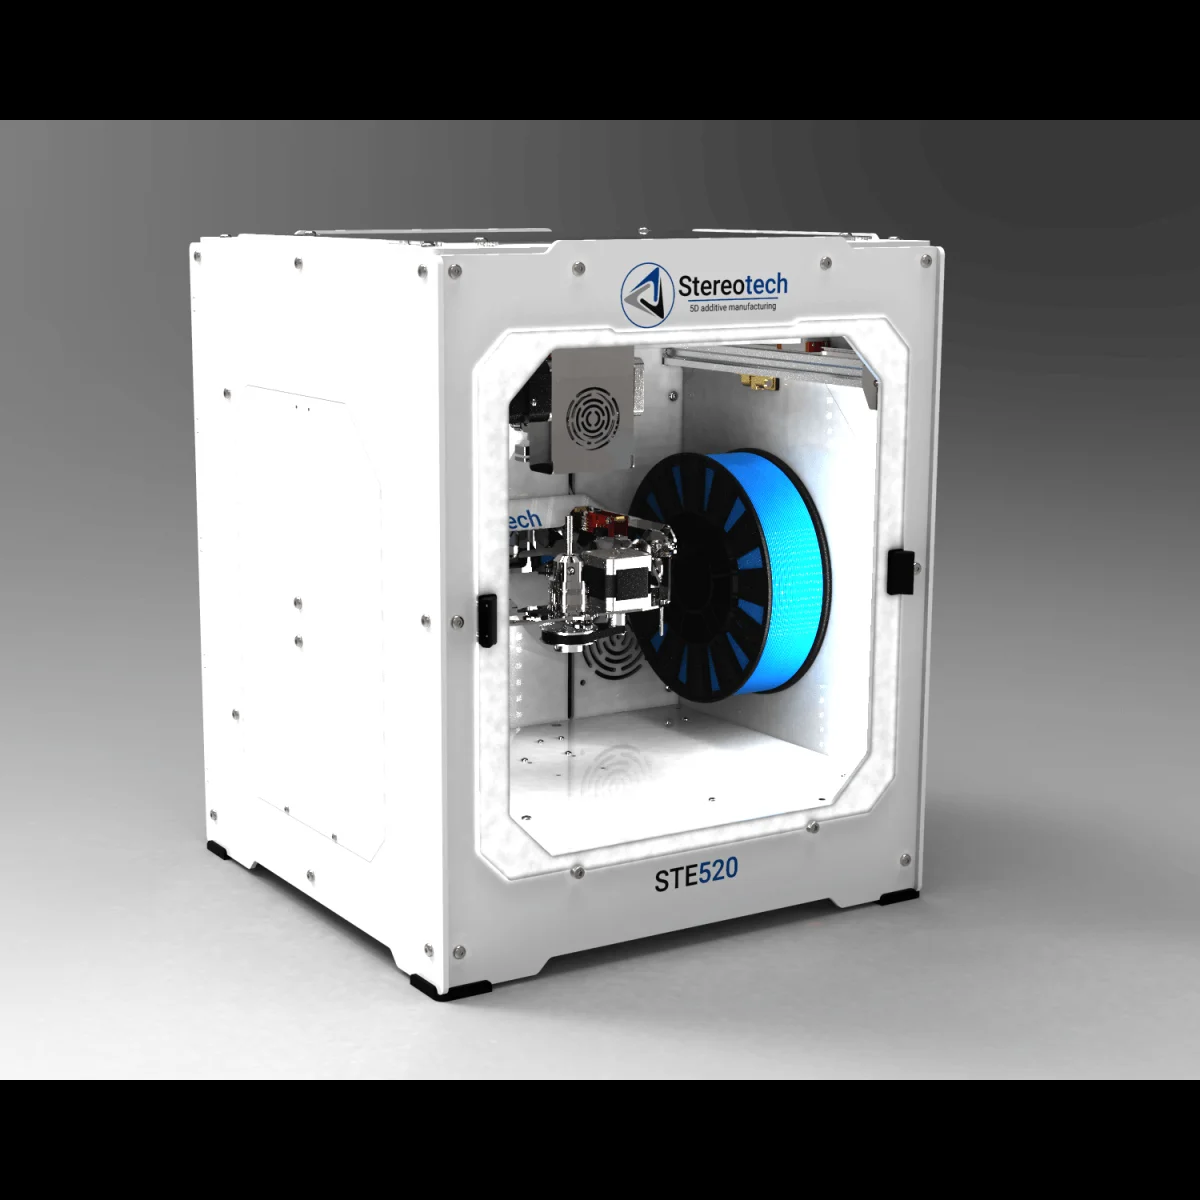
Спецификации
- Производител: Stereotech LLC.
- Технология: FDM
- Клас: experimenter
Чести проблеми и решения
Stringing
Thin, web-like plastic strands between different parts of the printed object caused by oozing from the nozzle. Решение: Dry the filament for 4-6 hours at 50°C for PLA or 70°C for Nylon. Increase retraction distance by 1-2 mm, lower the nozzle temperature by 5°C, and increase travel speed to 200 mm/s.
Warping
Corners or edges of the 3D print curl upwards and detach from the build plate due to uneven thermal contraction and residual stress. Решение: Increase the bed temperature by 5°C, use a 5-10 mm Brim, and apply bed adhesives like glue stick. Use an enclosure for materials like ABS and reduce part cooling to 30% for the first 5 layers.
Layer Shift
Horizontal misalignment of the upper printed layers compared to the lower layers. Решение: Tighten the mechanical drive belts, check the grub screws on pulleys, verify linear bearings, and reduce the printing speed by 20% to prevent stepper motors from skipping steps.
Under-extrusion
The printer supplies insufficient plastic, resulting in thin, brittle walls and structural gaps in the print. Решение: Perform a ‘Cold pull’ to clear partial nozzle clogs, calibrate extruder E-steps via M92 command, increase nozzle temperature by 5°C, and check extruder gear tension.
Clogging
Complete cessation of material extrusion during printing due to debris, heat creep, or moisture expansion inside the hot end. Решение: Execute the ‘Cold pull’ procedure 3-5 times. Check the heat break cooling fan, replace the PTFE tube if thermally deformed, and limit retraction to under 2 mm for all-metal hot ends.
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии
Обновено на 21 септември 2026
Този текст е написан с помощта на AI; фактите са сверени с източниците на 21 септември 2026.