
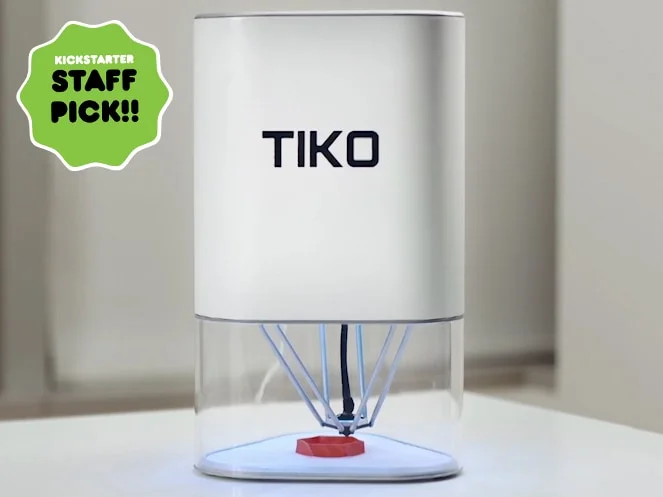
Спецификации
- Производител: Key3D
- Технология: FDM
- Клас: experimenter
Чести проблеми и решения
Stringing
Thin, web-like plastic strings appearing between separate parts of the print due to oozing during non-print travel moves. Solution: Dry the filament for 4-6 hours at 50-70°C, increase retraction distance by 1-2 mm, and reduce nozzle temperature by 5°C. Решение:
Warping
Corners or edges of the printed part lifting and curling away from the build plate due to thermal shrinkage and uneven cooling. Solution: Increase bed temperature by 5°C, use a 5-10 mm brim, utilize a closed enclosure, and reduce part cooling for the first 5 layers. Решение:
Under-extrusion
Thin, brittle walls and structural gaps in the printed part caused by insufficient material flow or partial clogging of the hotend. Solution: Perform a cold pull to clean the nozzle, calibrate extruder E-steps, and check the extruder gear tension to ensure teeth are properly biting into the filament. Решение:
Подходящи приложения
- Rapid Prototyping: Fast production of physical models to verify shape, fit, and ergonomics before mass production in Product Design workflows.
- Jigs and Fixtures: Creating custom manufacturing aids, templates, and holding tools subjected to mechanical loads within Automotive Manufacturing assembly lines.
- Custom Electronic Enclosures: Small-batch production of functional, custom-designed housings for smart devices and PCBs in the Consumer Electronics sector.
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии
Обновено на 21 септември 2026
Този текст е написан с помощта на AI; фактите са сверени с източниците на 21 септември 2026.