

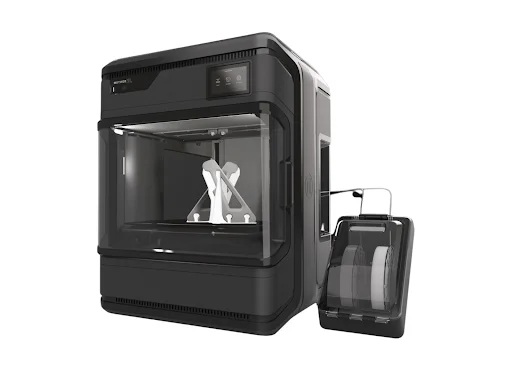
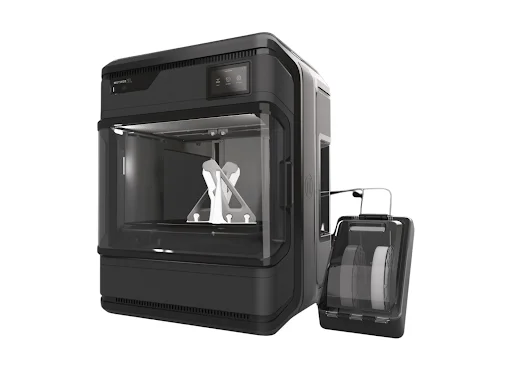
Спецификации
- Производител: Ultimaker B.V.
- Технология: FDM
- Клас: experimenter
Чести проблеми и решения
Stringing
Thin, web-like plastic strands appearing between separate parts of the print, primarily caused by hygroscopic filament absorbing moisture. Решение: Dry the filament for 4-6 hours (e.g., 50°C for PLA or 70°C for Nylon), increase retraction distance by 1-2 mm, reduce nozzle temperature by 5°C, and increase travel speed to 200 mm/s.
Warping
The corners or edges of the printed part lift off the build plate due to uneven thermal contraction and residual stress, especially common with engineering polymers. Решение: Keep the printer’s enclosure closed to maintain ambient temperature, increase the heated bed temperature by 5°C, add a 5-10 mm brim, and apply bed adhesives like Magigoo or a glue stick.
Under-extrusion
The appearance of thin, brittle walls and structural gaps in the model due to a partially clogged nozzle or incorrect extruder feeding rates. Решение: Perform a ‘Cold pull’ procedure to clear partial clogs, calibrate the extruder E-steps, and increase the nozzle temperature by 5°C.
Elephant’s Foot
The lowest layer of the print expands horizontally beyond the intended CAD dimensions because the first layer is squished too firmly against the heated bed. Решение: Increase the Z-offset by +0.05 mm, decrease the bed temperature by 5°C for the initial layer, and apply a software ‘Elephant foot compensation’ of 0.1-0.2 mm in the slicer.
Подходящи приложения
- Jigs and Fixtures: (Automotive and Heavy Manufacturing): On-demand manufacturing of specialized alignment tools, manufacturing aids, and templates using strong engineering materials like CF-Nylon or PC.
- Rapid Prototyping and Fit-checks: (Consumer Electronics and Product Design): Iterative printing of highly accurate models to validate form, ergonomic design, and mechanical assembly tolerances before mass production.
- Complex End-Use Components: (Aerospace and Industrial Engineering): Leveraging dual extrusion capabilities to print complex, ready-to-use functional geometries using soluble support materials like PVA or HIPS.
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии