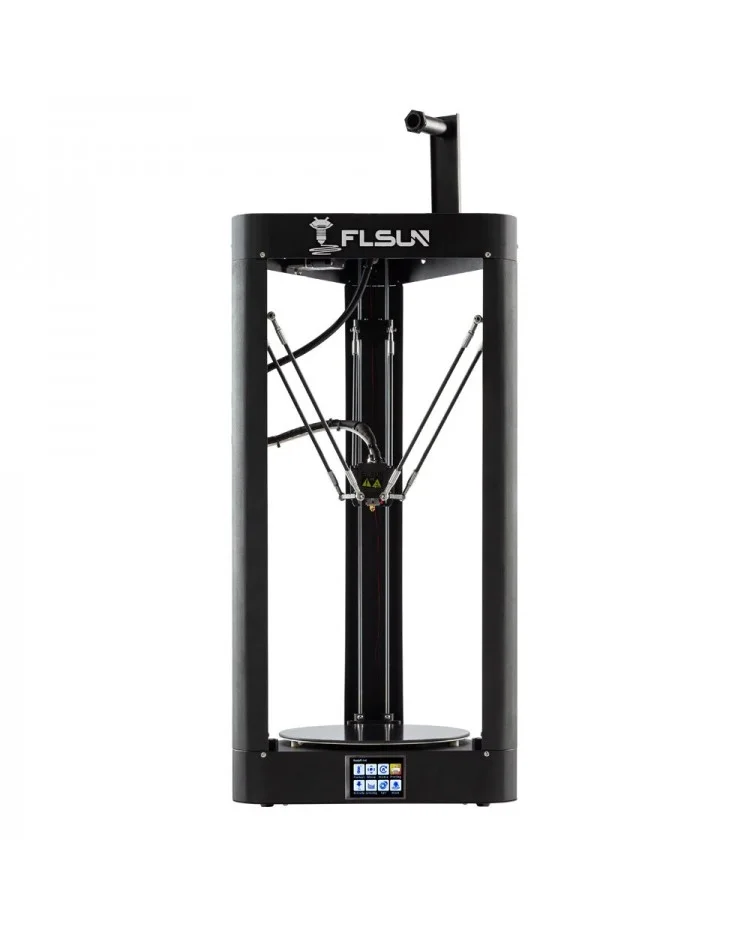
Спецификации
- Производител: Flsun
- Технология: FDM
- Клас: hobby
Чести проблеми и решения
Stringing
Thin, web-like plastic strands appearing between separated parts of the print, typically caused by moisture in the filament or insufficient retraction settings. Решение: Dry the filament for 4-6 hours at 50°C (for PLA) or 70°C (for Nylon), increase the retraction distance by 1-2 mm, and decrease the nozzle temperature by 5°C.
Layer Shift
Sudden horizontal displacement of layers during printing, a common issue in Delta kinematics if the long vertical belts are not tensioned evenly. Решение: Manually tighten the three drive belts on the vertical towers, check the grub screws on the stepper motor pulleys, and reduce print speed by 20%.
Bed Adhesion Fail
The first layer fails to stick to the build plate or detaches mid-print, often due to an improperly calibrated Z-offset or a contaminated glass/PEI bed. Решение: Clean the heated bed thoroughly with isopropyl alcohol (IPA), apply an adhesive like a glue stick, and fine-tune the Z-offset.
Подходящи приложения
- Rapid Prototyping: Producing quick physical models to verify shape, fit, and ergonomics within hours rather than days.
- STEM Demonstrations: Utilizing the visually engaging, tall Delta architecture of the printer to demonstrate robotics and additive manufacturing principles.
- Custom Tooling (Jigs & Fixtures): Manufacturing small batches (1-100 units) of custom assembly templates and holding fixtures in materials like PETG or ABS.
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии
Обновено на 21 септември 2026
Този текст е написан с помощта на AI; фактите са сверени с източниците на 21 септември 2026.