
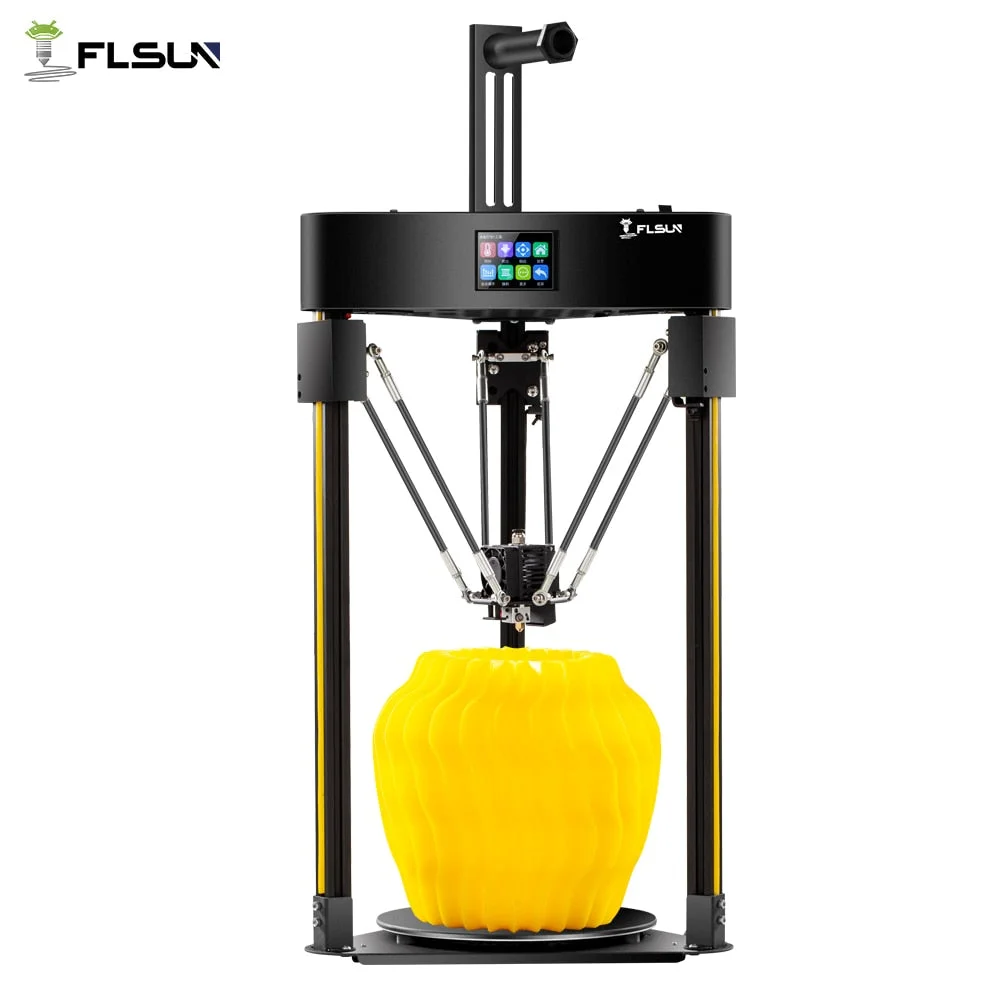
Спецификации
- Производител: Flsun
- Технология: FDM
- Клас: hobby
Чести проблеми и решения
Stringing
Thin webs or ‘spiderwebs’ of plastic between print sections. This is a common issue with the Flsun Q5 due to its long Bowden tube extruder setup. Решение: Dry the filament (e.g., 4-6 hours at 50°C for PLA), increase retraction distance by 1-2 mm, and decrease nozzle temperature by 5°C.
Layer Shift
A sudden horizontal displacement of printed layers, often caused by the high movement speeds of the Delta kinematics or loose belts. Решение: Check and evenly tighten the belts on all three vertical towers, tighten the grub screws on the stepper motor pulleys, and reduce print speed by 20%.
Under-extrusion
The printer extrudes too little plastic, resulting in weak, brittle walls or gaps, often caused by heat creep or Bowden tube friction. Решение: Perform 3-5 ‘cold pulls’ to clear the nozzle, calibrate the extruder E-steps (M92 command), and ensure the PTFE Bowden tube is fully seated against the nozzle.
Подходящи приложения
- Rapid Prototyping of Tall Geometries: Taking advantage of the Delta printer’s naturally high Z-axis capability to quickly print tall prototypes like bottles, vases, and enclosures.
- STEM Demonstrations: Utilizing the visually captivating movement of the three parallel articulating arms to teach coordinate geometry, kinematics, and basic robotics.
- Cosplay and Props Production: Creating lightweight, tall prop pieces at high speeds, minimizing the production time required for complex costume accessories.
Интерактивен Анализатор за Flsun q5 technical review – спецификации и настройки
Избери профил за да видиш детайлен анализ.
Инженер, автор на „Голямата книга на 3D принтирането“ и експерт по адитивни технологии
Обновено на 21 септември 2026
Този текст е написан с помощта на AI; фактите са сверени с източниците на 21 септември 2026.